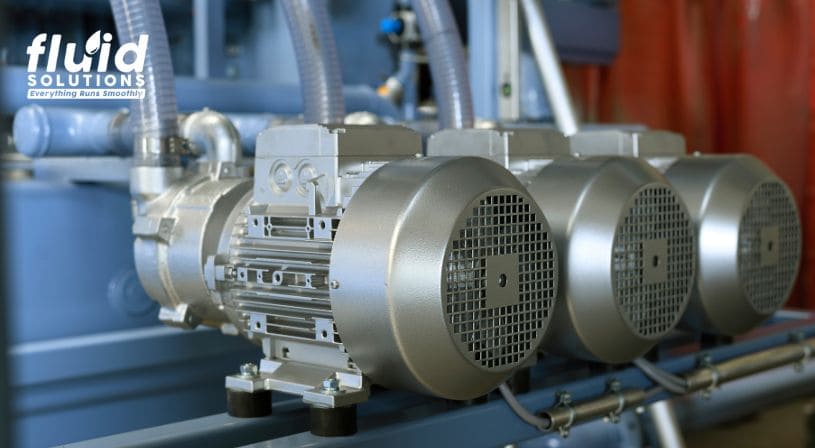
The oil you choose for your vacuum pump directly affects its performance, reliability, and service life. A proper vacuum pump oil lubricates moving parts to reduce wear, cools internal components, and seals the system to maintain proper vacuum levels. Using the right oil ensures consistent operation, while an incorrect choice can impair performance and shorten pump life.
This guide explains the key properties to consider and the different types of vacuum pump oils available, so you can make the most informed decision for your equipment.
Key Properties for Pump Oils Selection
Understanding their key properties helps users select the most apt and best oil for vacuum pumps to ensure smooth operation and prevent untimely damage.
- Viscosity: Impacts how well the oil flows and protects components.
- Operating Temperature Range: Oils must remain stable in both high-heat and low-temperature conditions.
- Chemical Compatibility: Oils should resist reacting with the gases or vapors being pumped.
- Vapor Pressure or Volatility: Low-volatility oils help maintain vacuum levels and prevent contamination.
- Service Life: Longer-lasting oils reduce downtime and maintenance costs.
Common Types of Vacuum Pump Oils
The key properties vary among the common types of vacuum pump oils, each possessing distinct strengths and limitations. Understanding these differences will help users select the most befitting type for their application.
Mineral Oils
Mineral oil is the most common and cost-effective vacuum pump oil, refined from crude oil and suitable for general-purpose applications.
- Viscosity: Its viscosity typically ranges from ISO VG 32 to 68
- Operating Temperature Range: It operates effectively within a temperature range of approximately 0°C to 160°F (32°F to 70°C).
- Chemical Compatibility: Mineral oil offers good compatibility with elastomers and moderate resistance to hydrolysis.
- Volatility: It has higher volatility compared to synthetic oils, making it prone to oxidation and sludge formation.
- Service Life: Mineral oils generally have a shorter service life and require more frequent oil changes.
Synthetic Oils
Synthetic oils are chemically engineered to deliver superior thermal stability, oxidation resistance, and low volatility.
- Viscosity: Typically ISO VG 32 to 68, with some customized grades.
- Operating Temperature Range: Operates effectively between approximately -20°C and 200°F (-4°F to 93°C).
- Chemical Compatibility: Exhibits excellent resistance to chemicals and hydrolysis, with good elastomer compatibility.
- Volatility: Low volatility with minimal sludge formation.
- Service Life: Provides the longest service life among common vacuum pump oils and supports extended oil change intervals.
Semi-Synthetic Oils
Semi-synthetic oils are blends of mineral and synthetic bases enhanced with additives to improve stability and performance.
- Viscosity: Similar to mineral oils, generally ISO VG 32 to 68.
- Operating Temperature Range: Typically effective from approximately 0°C to 160°F (32°F to 70°C).
- Chemical Compatibility: They provide better chemical stability than mineral oils.
- Volatility: Semi-synthetic oils exhibit lower volatility than mineral oils, reducing sludge formation.
- Service Life: They offer a longer service life compared to mineral oils.
PFPE (Perfluoropolyether) Oils
PFPE oils are highly specialized synthetic lubricants known for exceptional chemical inertness and outstanding thermal stability.
- Viscosity: Typically ranges from ISO VG 46 to ISO VG 150, varying by product and application.
- Operating Temperature Range: Effective from approximately -20°C to over 200°C (-4°F to 392°F).
- Chemical Compatibility: Outstanding chemical inertness; compatible with aggressive chemicals.
- Volatility: PFPE oils exhibit very low volatility.
- Service Life: This type of oil has a long service life, which is ideal for extreme conditions.
Ester Oils
Ester oils are synthetic lubricants offering good high-temperature performance and moderate compatibility with elastomers.
- Viscosity: The viscosity of ester oils typically ranges from ISO VG 32 to 68.
- Operating Temperature Range: They operate effectively within a temperature range of approximately -10°C to 200°C (14°F to 392°F).
- Chemical Compatibility: Provide moderate resistance to hydrolysis and have average compatibility with elastomer materials.
- Volatility: These oils exhibit moderate volatility under normal operating conditions.
- Service Life: Ester oils generally offer a moderate to long service life, which is better than mineral oils but usually shorter than synthetic oils.
Silicone Oils
Silicone oils are used in specialized vacuum pump applications requiring wide operating temperature ranges and chemical inertness.
- Viscosity: The viscosity varies but is generally low, averaging around ISO VG 10 to 50.
- Operating Temperature Range: They operate across a wide temperature range, from approximately -40°C to over 200°C (-40°F to 392°F).
- Chemical Compatibility: Provide moderate resistance to hydrolysis and have average compatibility with elastomer materials.
- Volatility: They exhibit low volatility during operation.
- Service Life: The service life is typically long, depending on the specific application.
Common Mistakes to Avoid
Avoid the following typical errors when selecting and using vacuum pump oils:
- Using general-purpose lubricants. Do not use ordinary lubricants. Use vacuum-rated oils made specifically for the pump.
- Ignoring OEM recommendations. Not adhering to the manufacturer’s instructions may cause damage or poor performance.
- Ignoring chemical exposure. Verify that the oils are suitable for the gases or vapors that the pump processes.
- Ignoring regular oil checks and replacements. Degraded oils can reduce pump life and efficiency.
- Oil grade does not match the operating temperature. Using oils that are not within its temperature range might lead to excessive wear or earlier breakdowns.
Get the Perfect Oil Match for Your Vacuum Pump with Fluid Solutions
Selecting the best vacuum pump oil means considering viscosity, temperature range, chemical compatibility, and service life, then matching the right type of oil to your application. Making the right choice helps ensure long-lasting, efficient, and trouble-free performance from your pump.
Fluid Solutions provides OEM-compliant vacuum pump oils and expert advice to help users choose the right option for their equipment in the Philippines. Whether you need oil for a specific pump or application, contact us at (02) 8370 5928 / (0917) 894 9156, or email us at [email protected]. Be sure to check out Facebook and LinkedIn pages for updates and product recommendations.